

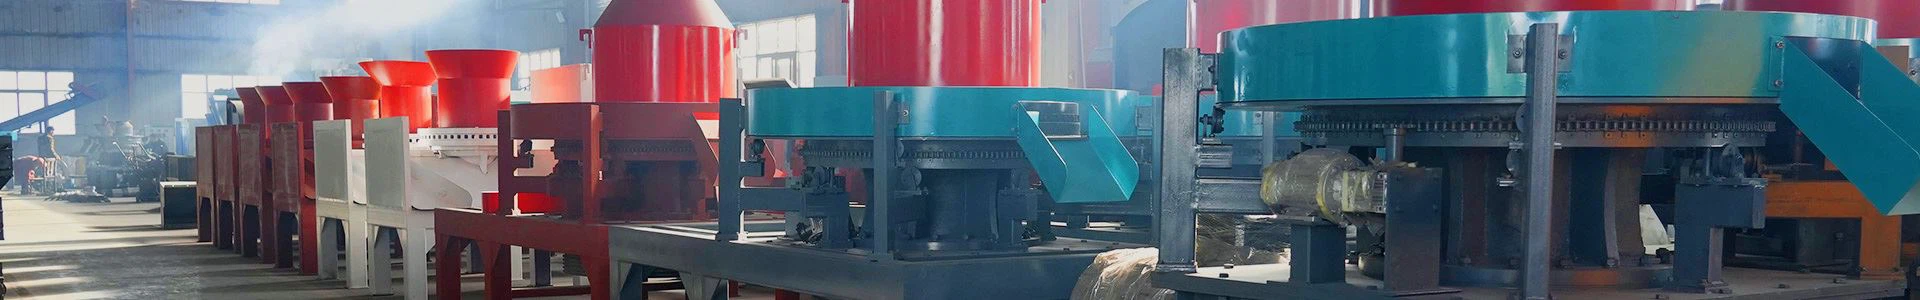
Wood Pellet Production Line Models and Cost Advantages for Biomass Fuel Plants
What a Wood Pellet Production Line Consists Of
A production line is a sequence of stages in which each one can limit the whole plant. Incoming material is reduced in size by a chipper or hammer mill, dried to the working moisture range, screened to remove oversize and contamination, metered into the pellet press, then cooled, screened again for fines and bagged or loaded in bulk. The press is the most visible item, but a line that has a 1.5 t/h press behind a dryer that can only remove 800 kg of water per hour will run at 800 kg/h. Sizing the stages to each other is the first cost decision in any project.
RKL Series Model Data
| Model No. | Capacity (kg/h) | Power (kW) | Weight (t) |
|---|---|---|---|
| RKL-250 | 100-200 | 15 | 0.5 |
| RKL-300 | 150-250 | 22 | 0.65 |
| RKL-350 | 100-300 | 30 | 0.76 |
| RKL-400 | 300-600 | 37 | 2.2 |
| RKL-450 | 500-800 | 55 | 4.3 |
| RKL-550 | 1000-1500 | 90 | 5.5 |
The range spans a factor of roughly ten in output. The RKL-250 and RKL-300 suit farm-scale or workshop production, the RKL-350 and RKL-400 cover the small commercial band, and the RKL-450 and RKL-550 are the entry point for continuous industrial production.
Cost Advantage 1: Specific Energy Falls as Capacity Rises
The installed power per tonne of output can be calculated directly from the table for the pelletizing stage alone. The RKL-550 at 90 kW and 1.0-1.5 t/h implies a pelletizing load of about 60 to 90 kWh per tonne, while the RKL-250 at 15 kW and 0.1-0.2 t/h implies 75 to 150 kWh per tonne at the same stage. This calculation excludes drying, conveying and cooling, but it shows the direction clearly: running a large press near the top of its capacity band is cheaper per tonne than running a small press at its limit, provided the upstream stages can supply it.
Cost Advantage 2: Uniform Product Reduces Losses Downstream
A production line produces pellets of consistent size, shape and density. Uniform pellets can be moved in bulk, stored in silos without segregation and burned at a steady rate in boilers and stoves, which gives a stable heat output. Consistency also reduces losses: fines generated during handling are a direct loss of saleable product, and pellet quality is graded for exactly this reason. Graded wood pellets for the traded market are specified in ISO 17225-2:2021, which defines classes A1, A2 and B with limits on moisture, ash and net calorific value, and uses designations such as D06 and D08 for the nominal diameter.
Cost Advantage 3: Low-Cost Feedstock and Value-Added Output
The economics of a pellet line rest on the gap between the price of the raw material and the price of the finished pellet. Sawdust, wood shavings, straw and rice husk are low-cost inputs that are often waste elsewhere in the value chain, and the press converts them into a product that can be traded by the tonne against a written specification. Efficient operation also spreads labour cost across more tonnes: the same two or three operators run a line at 1,500 kg/h that would be needed to run a line at 300 kg/h.
What Actually Drives Operating Cost per Tonne
Drying load: the moisture that has to be removed before pressing is usually the largest single energy item in the plant. Feedstock delivered dry is worth more than the same feedstock delivered wet, even at a higher purchase price.
Wear parts: die and roller life depends strongly on abrasive contamination. Screening before the press is cheaper than early die replacement.
Load factor: a line started and stopped repeatedly loses both throughput and die life. Steady feedstock supply and a buffer of dried material keep the press running at its design point.
Pellet quality losses: crumbled pellets and fines are product without a market, so press moisture and die condition have a direct commercial value.
Selecting a Line for a Given Output
Work backwards from the target annual tonnage. Divide it by the number of working hours, add the availability allowance for maintenance and feedstock interruptions, and select the press model whose upper capacity band exceeds that figure. Then size the dryer, the hammer mill and the conveyor to the press, not the other way round. Where feedstock supply is seasonal, planning for a larger buffer of dried material is usually cheaper than oversizing the press.
Frequently Asked Questions
Q: What is the capacity of the largest RKL model?
A: The RKL-550 runs at 1000-1500 kg/h with 90 kW installed power and a total weight of 5.5 t. The smallest model, the RKL-250, runs at 100-200 kg/h with 15 kW.
Q: What moisture content should the feedstock be before pelletizing?
A: A working range of about 12-15 percent suits most wood feedstocks. Damp material must be dried first, which is normally the biggest energy cost in the plant, so moisture control at the receiving point matters more than any machine setting.
Q: Do the models in the table represent the whole line or only the press?
A: The capacity, power and weight figures apply to the pelletizing unit. A complete line also includes chipping or grinding, drying, screening, cooling, fines screening and packing equipment, all of which must be sized to match the press.
Q: How is pellet quality specified for sale?
A: By the property limits of ISO 17225-2:2021 for graded wood pellets. Moisture is determined by the oven methods of ISO 18134, ash content by ISO 18122 and calorific value by ISO 18125; mechanical durability of pellets is determined by ISO 17831-1.
Q: Why does pellet uniformity affect cost as well as quality?
A: Uniform pellets handle in bulk without segregation and burn at a steady rate, so less product is lost as fines during storage and transport and complaints from boiler operators are fewer. Losses in handling are lost revenue.
Q: Which model suits a farm using its own sawdust?
A: For own-use production the RKL-250 to RKL-350 band at 100-300 kg/h is usually sufficient. The larger RKL-450 and RKL-550 models are intended for plants selling pellets in bulk on a commercial basis.


