

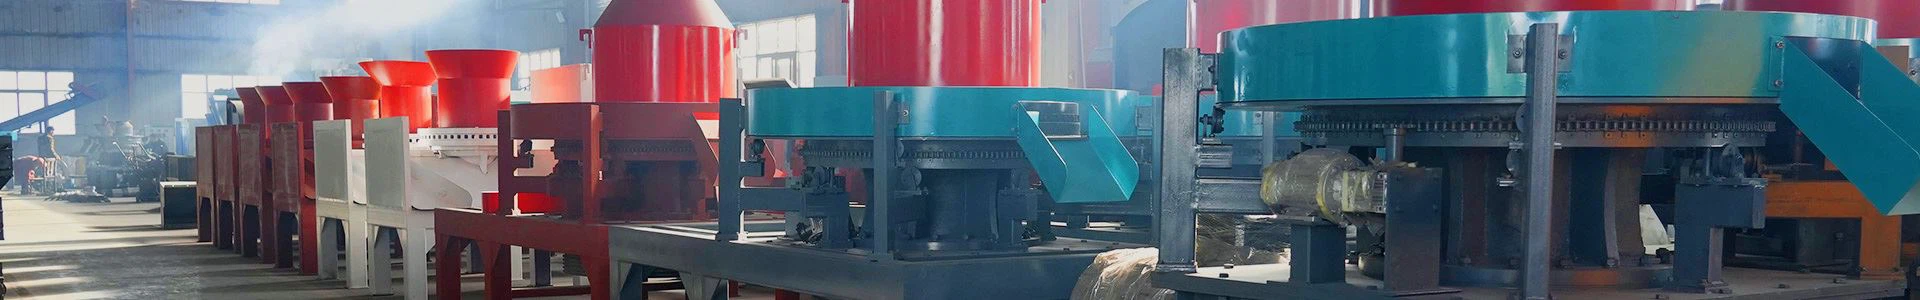
RDF Molding Machine Operating Techniques: Preheating and Two-Stage Feeding
What an RDF Molding Machine Does
An RDF molding machine is fuel-forming equipment that briquettes combustible solid waste which is loose in texture, low in calorific value and difficult to transport or store. The molding process compresses these materials into dense briquettes, cutting the volume and raising the heating value so that the product behaves much like coal.
Because of that coal-like performance, refuse-derived fuel briquettes are used in waste-to-energy plants, cement kilns and industrial boilers. For waste managers and plant operators, the machine converts a problematic waste stream into a storable, transportable fuel instead of sending it to landfill or to incineration without energy recovery.
The machine integrates four main mechanisms - the pressure roller, the forming mold, the anti-stuffing device and a fully automatic oil pump. The pressure roller forces material into the forming mold, the anti-stuffing device keeps loose fibrous material from accumulating at the feed point and interrupting production, and the oil pump maintains roller lubrication during long runs, which reduces wear and keeps production parameters stable.
Technical Parameters of Common Models
Production scale determines model choice. All models below produce a square 32 x 32 mm briquette profile, so the deciding factors are the required hourly output and the available power supply.
| Model | Power | Capacity | Briquette size | Die holes |
|---|---|---|---|---|
| MK-550 | 55 kW | 1.0-1.5 t/h | 32 x 32 mm | 36 |
| MK-750 | 75 kW | 1.5-2.0 t/h | 32 x 32 mm | 54 |
| MK-900 | 90 kW | 2.0-2.5 t/h | 32 x 32 mm | 72 |
| MK-1600 | 160 kW | 2.5-3.0 t/h | 32 x 32 mm | 120 |
Select a model whose capacity matches your material supply rate. Underfeeding wastes power and produces uneven briquettes, while overloading trips the drive and accelerates wear on the roller and mold.
Pre-Start Inspection Checklist
A short inspection before every shift prevents most startup failures and safety incidents. Work through the checks in order:
Confirm that all connecting parts are tightened reliably - a loose bolt can do serious damage once the machine runs at full speed.
Check for debris inside and around each part, and remove any metal fragments or hardened residue.
Check that bearings and lubricating points are not short of oil, and top up the automatic oil pump reservoir.
Confirm that the instruments in the control cabinet display normally, with no alarm or fault indication.
Inspect the electrical wiring for damage, including the cable entries and the motor terminal box.
These checks take only a few minutes but protect both the operator and the equipment.
Preheating and Two-Stage Feeding
An RDF molding machine must be preheated before production starts. Turn on the heating switch and let the temperature rise to about 100-120 °C before starting the machine. After the machine has run for one minute, material can be loaded.
The most important operating technique on a new startup is two-stage feeding:
Stage one: feed a small amount of material evenly, starting with material whose moisture content is above 40%. Continue until all die holes of the equipment are discharging. High-moisture material extrudes more easily and fills every hole, which establishes the extrusion condition.
Stage two: after about 10 minutes of discharge, with pressure and temperature parameters reading normally, switch to material with moisture below 20% and continue until discharge is steady. Then raise the feed to the target production rate.
Skipping the wet-material stage is a common cause of startup blockage, uneven briquettes and unnecessary roller wear, so treat it as a fixed procedure rather than an optional warm-up.
Running Checks and Between-Run Maintenance
During production, watch the die discharge pattern rather than the machine body. When every die hole discharges evenly and pressure and temperature remain stable, the machine is running correctly at the target feed rate. A single dry hole, a sudden rise in pressure or a drop in output all point to partial blockage or material that is too dry.
Between production runs, keep all connecting parts tight, remove debris from inside and outside the equipment, verify bearing lubrication, confirm that control cabinet instruments display normally, and inspect the electrical wiring. Keeping the anti-stuffing device clear is equally important on fibrous waste streams, because accumulated film or textile residue eventually reaches the roller and is compressed into hard patches that disturb the mold.
| Symptom | Likely cause | Action |
|---|---|---|
| Die holes not discharging at startup | Machine not preheated, wet stage skipped | Preheat to 100-120 °C and repeat the high-moisture stage |
| Briquettes uneven or weak | Material too dry or badly mixed | Adjust moisture and blend the waste stream more evenly |
| Pressure rising with falling output | Partial die blockage or foreign object | Stop, clear the mold and feed point, remove the obstruction |
| Material piling at the feed point | Anti-stuffing device fouled by fibrous waste | Clean the device and shorten the cleaning interval |
Frequently Asked Questions
Q: What raw materials can an RDF molding machine process?
Loose combustible solid waste, including paper-rich fractions, plastic film, textile waste and other high-calorific waste streams that are difficult to transport and store in loose form.
Q: Why must the equipment be preheated before starting?
Preheating to 100-120 °C softens the binding components in the waste and prepares the die. Starting cold tends to make material slip in the die holes, producing uneven briquettes or blockage.
Q: Why are high-moisture materials fed first during startup?
Material above 40% moisture extrudes more easily and fills all die holes quickly, establishing the extrusion condition. Once the holes are full, drier material below 20% moisture takes over for normal production.
Q: How do I know the machine is running normally after startup?
When all die holes discharge evenly and pressure and temperature stay stable after about 10 minutes of discharge, the machine is ready for continuous production at the target feed rate.
Q: How should the machine be maintained between production runs?
Keep connecting parts tight, clear debris inside and outside the equipment, check bearing and oil pump lubrication, verify control cabinet instruments and inspect the electrical wiring before each run.
Q: How is model size selected for an RDF briquetting line?
Match the rated capacity to your material supply rate and available power: the 55-90 kW models suit 1-2.5 t/h duties, while the 160 kW model covers 2.5-3 t/h, all producing a 32 x 32 mm briquette.


