

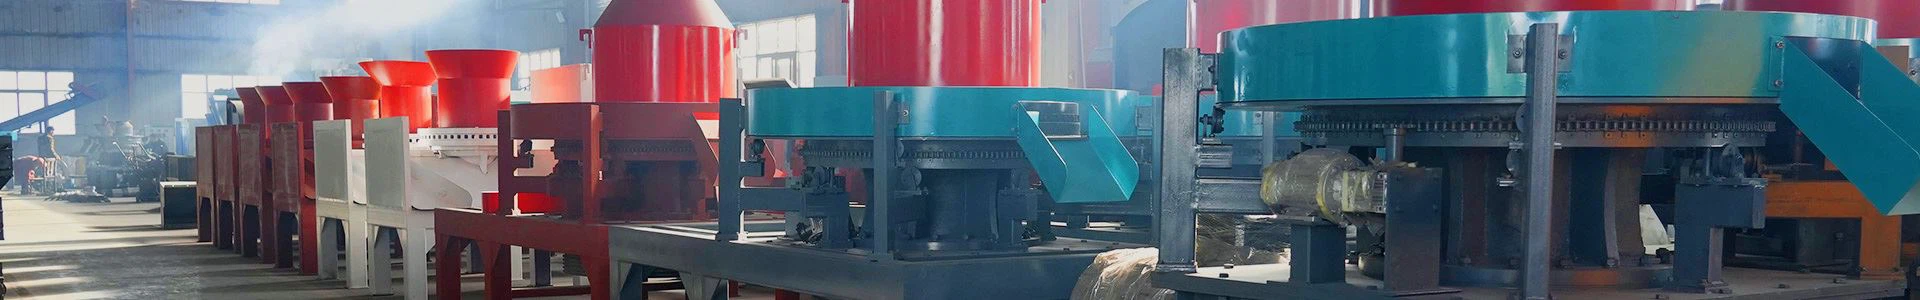
From Wood Chips to Pellet Fuel: How a Biomass Pellet Line Works
From Raw Material to Finished Pellet
The core components of a typical biomass pellet line are a grinder, a dryer, a pelletizer and a packaging machine. If the diameter of the raw material to be processed exceeds 100 mm, a chipper is also required. Working together, these machines form a complete production process that carries material from raw wood chips through to bagged pellet fuel.
Pellet quality is decided long before the material reaches the pelletizer. Every upstream stage removes one specific obstacle: the chipper and grinder control particle size, the dryer controls moisture, the pelletizer controls density, and the cooling and packaging stage protects the finished pellet from moisture regain and breakage. A line is only as good as its weakest step, so capacity has to be matched across all of them.
Preparation: Chipping, Pulverization and Drying
In the first stage, large wood chunks with diameters exceeding 100 mm to 220 mm are processed in a chipper to reduce them to strands smaller than 100 mm. This step is crucial for the smooth progress of the subsequent pelletizing stages, because the pulverizer cannot accept oversize pieces.
The pulverizer is designed to finely reduce wood strands with diameters ranging from 10 mm to 100 mm into sawdust at the particle size the die requires. An even, fine grind is what ensures the ideal raw material quality: coarse particles produce weak pellets with rough surfaces, while consistent fines produce a dense, uniform product.
The dryer then removes surplus water from sawdust with a moisture content above 20 percent. The goal is to hold moisture within the optimal range of 10 percent to 15 percent so that pelletizing runs smoothly. Material that is too wet flashes to steam inside the die and produces soft, cracked pellets, while material that is too dry lacks sufficient natural binder and consumes extra energy per ton.
Pelletizing, Cooling and Packaging
The biomass pelletizer processes the dried sawdust, at a moisture content of 10 percent to 15 percent, into renewable biomass pellets suitable for direct combustion. The die and pressure rollers compact the material, and the friction generated inside the die softens the natural lignin of the wood so that the fibres bond together without any external additive.
After pelletizing, the pellets are stored in a cooling silo to ensure quality and extend their lifespan. The pellets are cooled rapidly in the silo before being finely packed by a baler for easy storage and transportation. Rapid cooling matters because hot pellets are soft and release moisture as they cool; packing them warm would trap that moisture inside the bag and cause mould and crumbling in storage.
Pellet Line Equipment Specifications
The table below lists the published specifications of the pelletizer series, including motor power, die hole quantity, capacity and pellet size.
| Model | Power | Mold hole | Capacity for industrial solid (t/h) | Capacity for biomass (t/h) | Pellet size (mm) |
|---|---|---|---|---|---|
| MKYK-36 | 45 kW | 36 | 0.5 - 1.0 | 1.0 - 1.5 | 32 x 32 x 50 - 100 |
| MKYK-48 | 75 kW | 48 | 1.0 - 1.5 | 1.5 - 2.5 | 32 x 32 x 50 - 100 |
| MKYK-72 | 110 kW | 72 | 2.0 - 2.5 | 2.5 - 3.5 | 32 x 32 x 50 - 100 |
| MKYK-90 | 132 kW | 90 | 2.0 - 2.5 | 3.5 - 5.0 | 32 x 32 x 50 - 100 |
| MKYK-120 | 200 kW | 120 | 3.0 - 4.0 | 4.0 - 6.0 | 32 x 32 x 50 - 100 |
| MKYK-150 | 250 kW | 150 | 4.0 - 6.0 | 6.0 - 10.0 | 32 x 32 x 50 - 100 |
Capacity depends on the feedstock. Loose, light biomass such as straw and sawdust runs at higher output than dense industrial solid residues of the same die, which is why the series publishes two capacity columns. When sizing a line, start from the moisture-adjusted output that the grinder and dryer can actually deliver, then select the pelletizer so that the press is the last machine to reach its limit rather than the first.
Line Monitoring and Process Stability
A stable pellet line is built around stable inputs. The system monitors the production situation in real time so that all operating parameters stay within their set range, which improves accuracy and stability. Operators watch three numbers above all others: the load on the main motor, the feed moisture, and the temperature of the die.
Motor load - a rising load with steady feed signals a worn die or a blocked hole.
Feed moisture - drift outside 10 to 15 percent changes density and increases fines.
Die temperature - the die must stay warm enough to soften lignin but not so hot that the wood scorches.
Screening after cooling removes the fines generated during handling and returns them to the pelletizer, so the only material leaving the line is finished, saleable pellet fuel.
Frequently Asked Questions
Q: What equipment makes up a complete biomass pellet line?
A chipper when the raw material exceeds 100 mm, a grinder, a dryer, a pelletizer, and a cooling and packaging stage, linked by conveyors and controlled as one process.
Q: Why is a chipper needed before the pulverizer?
Chunks from 100 mm to 220 mm are first cut into strands smaller than 100 mm, because the pulverizer reduces material only between 10 mm and 100 mm into sawdust.
Q: What moisture content does the dryer target?
Material entering at above 20 percent moisture is dried to the 10 to 15 percent range that allows smooth pelletizing and dense pellet formation.
Q: Why must pellets be cooled before packaging?
Hot pellets are soft and still releasing moisture. Rapid cooling in a silo hardens them and prevents mould and crumbling once the bags are sealed.
Q: Why are there two capacity columns in the specification table?
Dense industrial solid residues run at lower output than light biomass on the same die, so the series is rated separately for each material group.
Q: How is pellet size controlled?
Pellet size is set by the die profile and the cutter position. The published profile for the series is 32 x 32 mm with lengths between 50 mm and 100 mm.


