

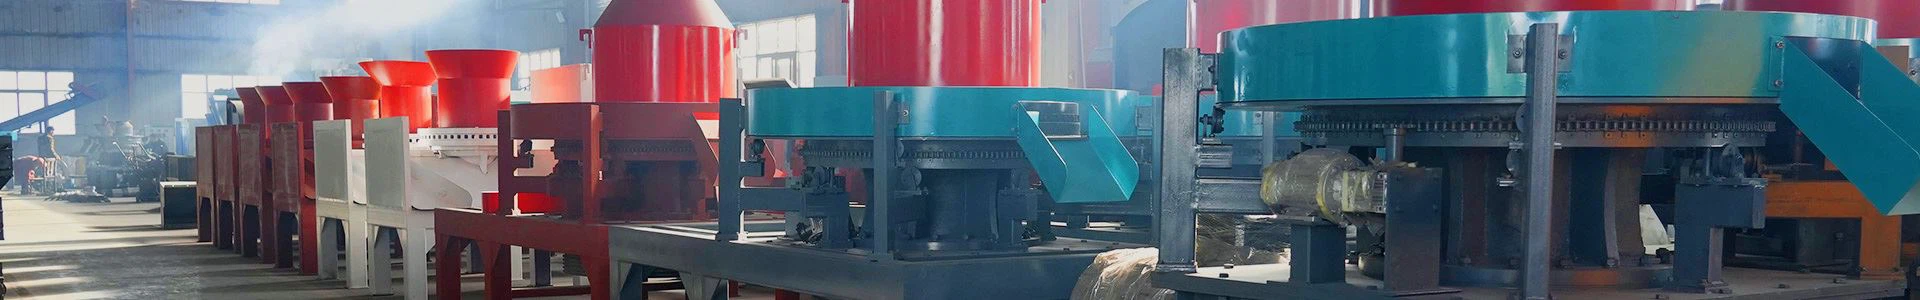
How Does a Wood Chip Charcoal Extruder Operate?
The Role of the Extruder in Charcoal Production
A wood chip charcoal extruder, also called a sawdust log making machine or briquette press, compresses loose sawdust into dense cylindrical rods before the carbonization step. Direct carbonization of loose sawdust results in high material losses of over 20 percent, uneven carbonization, and easy agglomeration of the particles. The extrusion principle of the briquetting machine solves these problems by giving the carbonization furnace a uniform, dense feedstock.
The extruder works by pushing the pre-treated raw material into a narrow molding cavity under high pressure. The compressed rod has a much higher density than loose sawdust, so the raw material distributes evenly inside the carbonization machine, heat conduction becomes more efficient, and carbonization losses can be controlled within about 8 percent.
The Extrusion and Densification Process
In a typical screw extrusion charcoal briquette machine, the pre-treated sawdust enters the feed inlet and is pushed forward by the rotating screw shaft into a narrowing molding chamber. An external heating device softens the lignin in the material, which acts as a natural binder, while the screw shaft continuously builds up pressure. The material is extruded from the molding sleeve as a dense rod and then cut into finished logs of a set length by a cutter.
Compressing sawdust into rods increases the density to about 1.0 to 1.2 grams per cubic centimeter. At this density the rods hold their shape, stack well in the carbonization furnace, and burn evenly, which significantly improves the utilization of the raw material.
How Extrusion Improves Charcoal Quality
The sawdust log making machine produces briquettes with a dense fiber structure. Inside the carbonization machine, the volatile matter is discharged more completely from the dense rod than from loose sawdust. As a result, the fixed carbon content of the finished charcoal is typically 10 to 15 percent higher than charcoal made from carbonized loose sawdust.
This denser structure also raises the calorific value to about 6000 to 7000 kilocalories per kilogram and extends the combustion time of the finished charcoal by 2 to 3 hours. For end users such as restaurants, barbecue shops, and industrial heating customers, longer burning time and higher heat output mean better value and more stable operation.
Matching the Extruder to the Carbonization Line
A carbonization machine needs continuous feeding to run efficiently. The continuous extrusion principle of the briquette machine matches the operating rhythm of the carbonization machine: a small briquetting machine produces roughly 500 to 1000 kilograms of sawdust briquettes per hour, which matches the feeding requirement of a carbonization machine of the same size. This avoids the efficiency drop caused by frequent start-ups and shutdowns of the carbonization furnace.
When the two machines work together in a continuous briquetting-and-carbonization operation, the daily processing capacity can increase by about 40 percent compared with batch processing. This arrangement suits medium and large scale production scenarios where throughput and labor efficiency are important.
Adjusting Product Size and Operating Points
The extruder can change the specifications of the sawdust charcoal briquettes by replacing the molding sleeve and cutter settings. This ensures uniform briquette size after carbonization, eliminates the need for secondary screening, and directly adapts the output to the requirements of the buyer or of downstream processing.
For stable operation, the raw material moisture should be kept in the recommended range, typically 8 to 12 percent, and the particle size should be fine enough to feed evenly into the screw. Check the clearance between the screw and the molding sleeve before starting, and preheat the heating device to the set temperature before feeding. If the rod surface comes out rough, adjust the heating temperature or the material moisture, and if the machine jams, stop it immediately for cleaning.
Frequently Asked Questions
Q1: Why must sawdust be compressed before carbonization?
Loose sawdust causes losses of over 20 percent during carbonization and carbonizes unevenly. Compressed rods carbonize uniformly and reduce losses to roughly 8 percent.
Q2: What density should the extruded rods have?
Typical density after extrusion is 1.0 to 1.2 grams per cubic centimeter, which is dense enough to hold the shape and burn evenly in the carbonization furnace.
Q3: How much does extrusion improve the calorific value of charcoal?
Charcoal from extruded rods typically reaches 6000 to 7000 kilocalories per kilogram, with a fixed carbon content 10 to 15 percent higher than charcoal from loose sawdust.
Q4: Can one extruder supply a carbonization machine continuously?
Yes. A small briquetting machine producing 500 to 1000 kilograms per hour matches the feeding rate of a same-size carbonization machine, enabling continuous operation.
Q5: What moisture content is suitable for the sawdust before extrusion?
Keep the moisture in the range of 8 to 12 percent. Material that is too wet slips in the molding chamber, while material that is too dry produces cracked rods.
Q6: How do I change the size of the charcoal briquettes?
Replace the molding sleeve and adjust the cutter setting on the extruder. After carbonization the briquettes keep a uniform size, so no secondary screening is needed.


